Modified & Colored EVA Compounds for Every Application
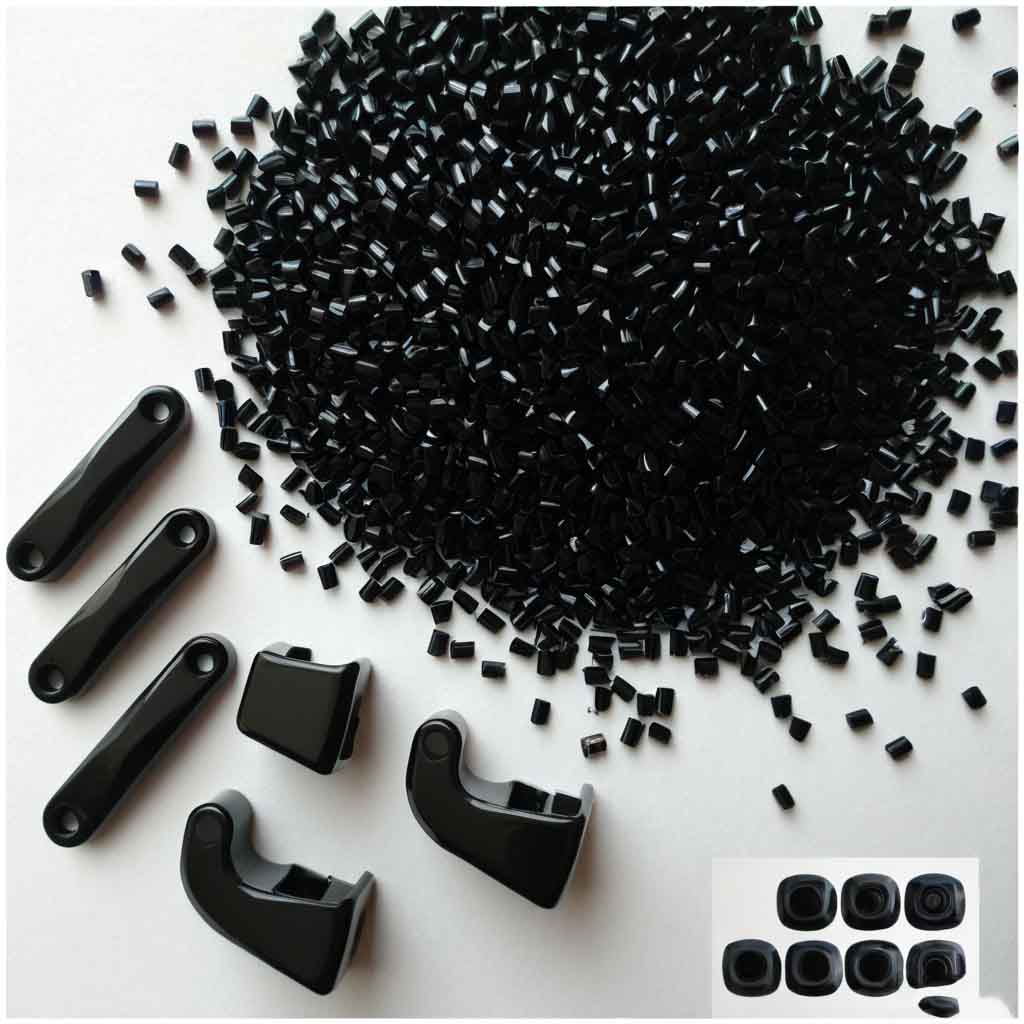
Modified EVA Compounds and Colored EVA Compounds expand the application scope of ethylene-vinyl acetate copolymer in two key dimensions: performance and appearance. Through tailored formulation, the modified grade provides enhanced elasticity, thermal stability, and heat shrink performance; the colored grade ensures consistent color delivery and batch uniformity. Both are widely used in footwear, cable, consumer goods, sporting goods, and medical applications, addressing both functional and aesthetic requirements across industries.
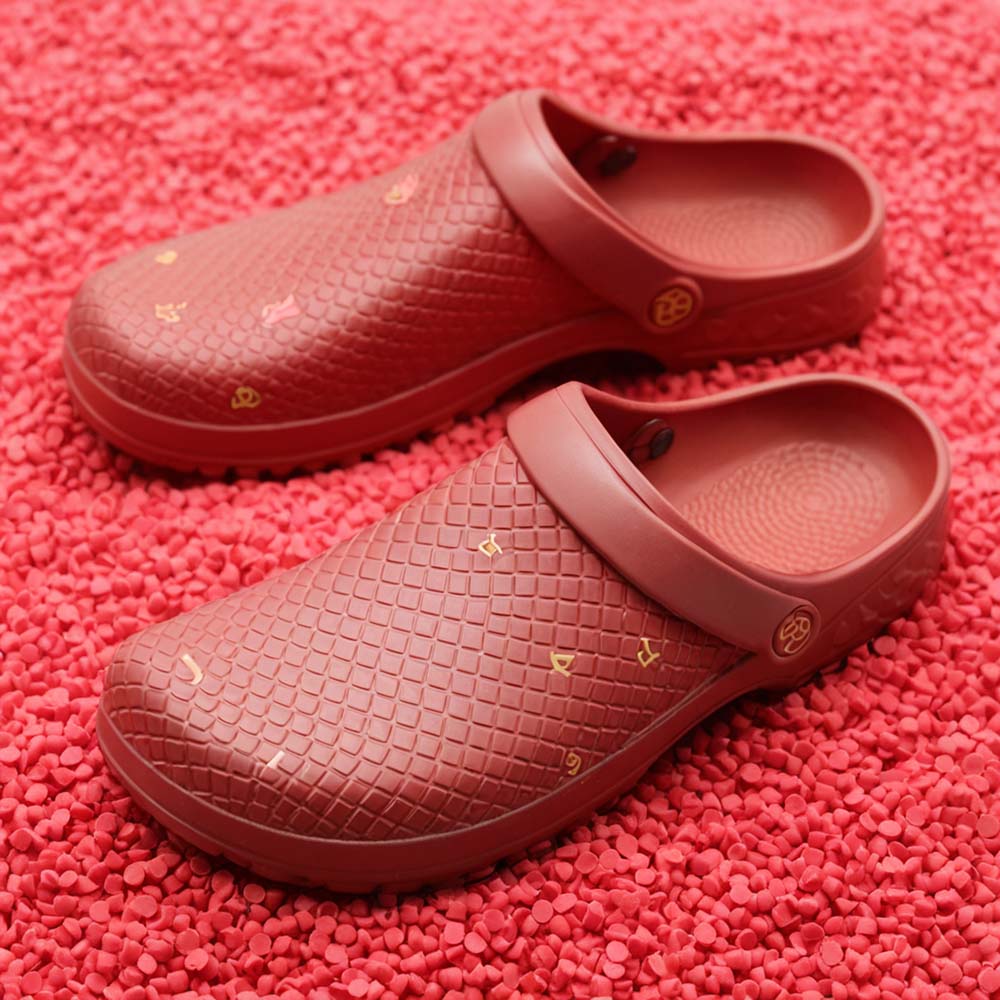
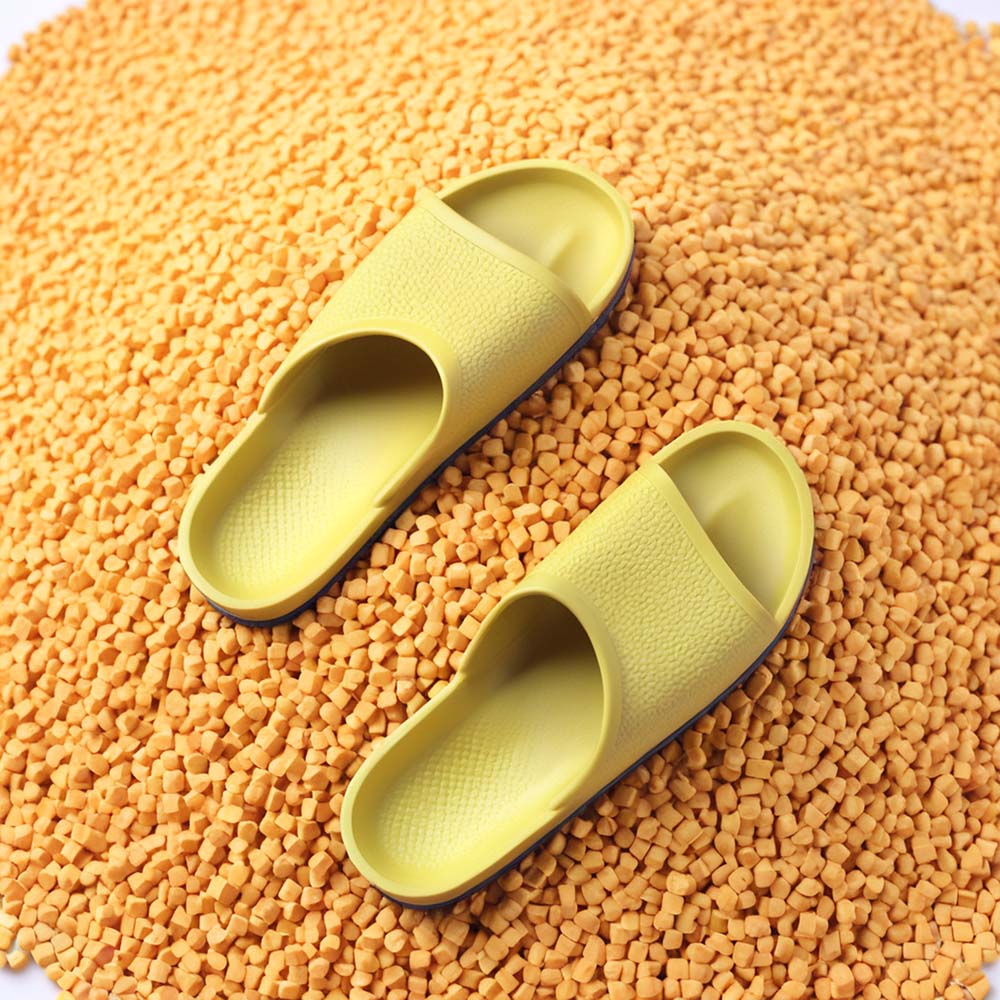
EVA Masterbatch For Slippers
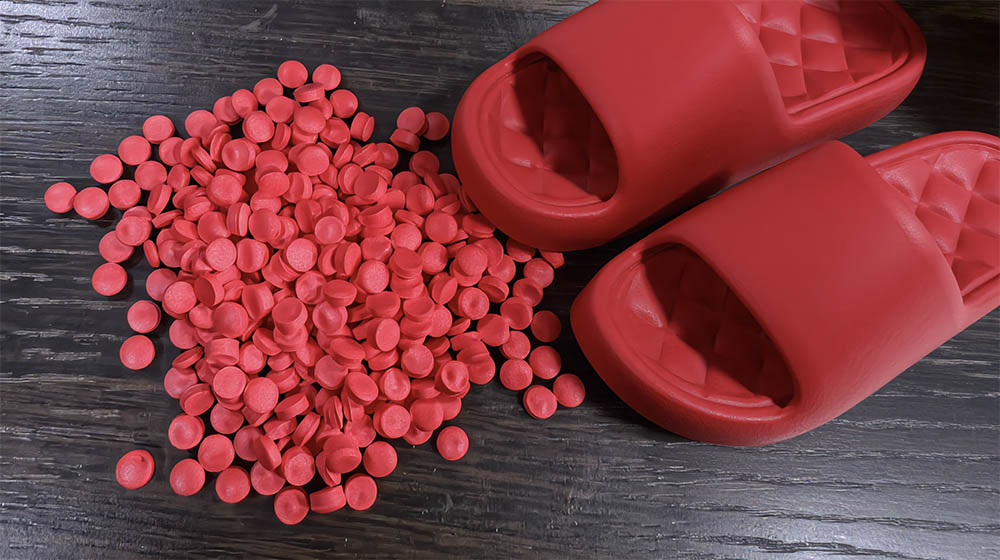
EVA compound for slippers is engineered with lightweight softness as the core advantage. The low density ensures each pair stays lightweight without tiring feet; the soft and comfortable texture provides a warm tactile feel. With excellent flow properties, the material enables smooth injection molding and foam expansion, delivering high production efficiency. The finished product offers superior resistance to bending and cracking, making it ideal for household slippers, beach sandals, disposable slippers, and more.
EVA Material For Soles
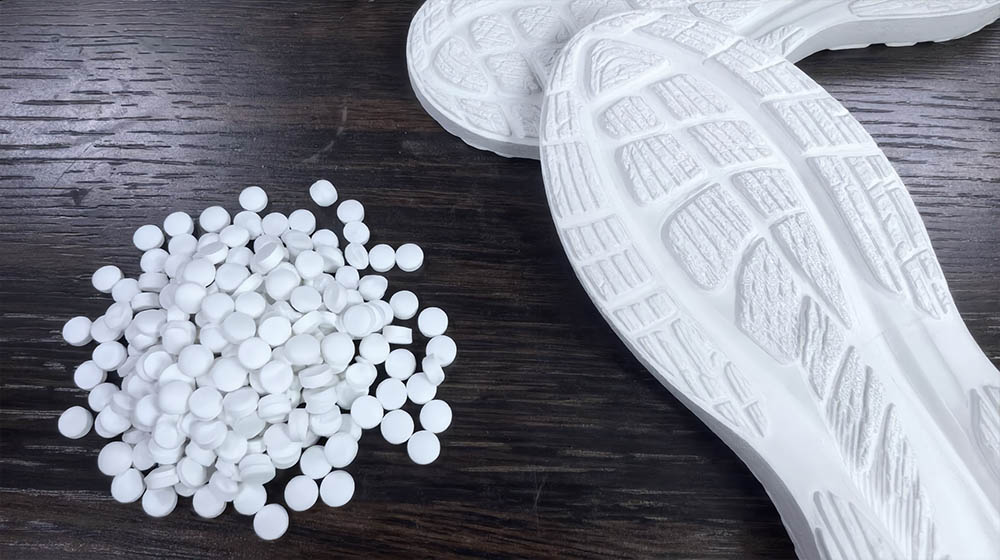
EVA A Grade material for shoe soles features high resilience and durability as its core advantages. The material delivers outstanding rebound performance with comfortable foot feel and clear energy return. Enhanced abrasion and flex resistance significantly extend the service life of shoe soles, preventing cracking and delamination. Ideal for brand footwear, 】and a wide range of sport and casual shoe sole applications.
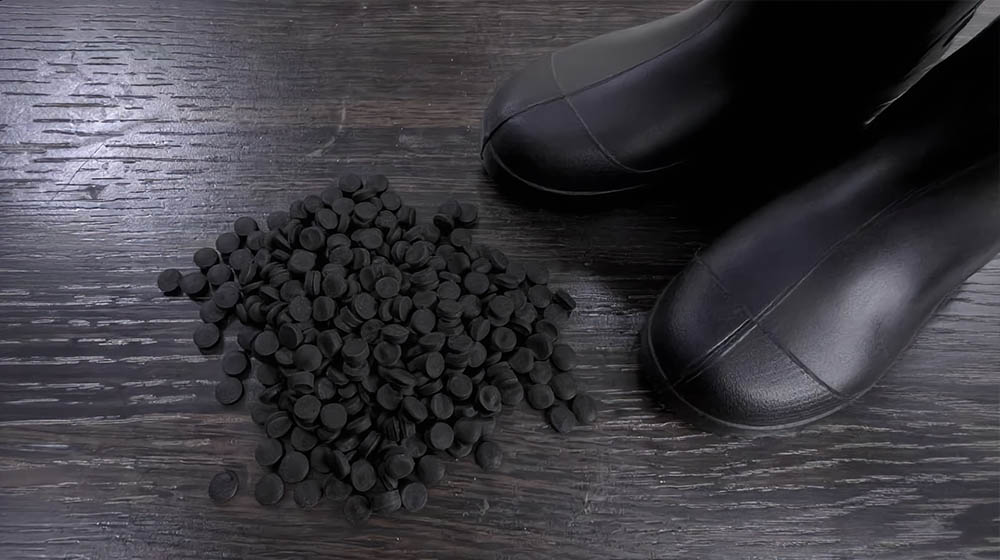
EVA Material For Boots
EVA compound for boots delivers exceptional compressive strength, withstanding sustained pressure and deformation from boot shaft structures. Outstanding abrasion, oil, and hydrolysis resistance ensures reliable performance in harsh environments such as moisture and oil exposure. The finished product maintains a firm and structured shape without collapsing or deforming. Ideal for industrial boots, rain boots, outdoor boots, snow boots, and more.
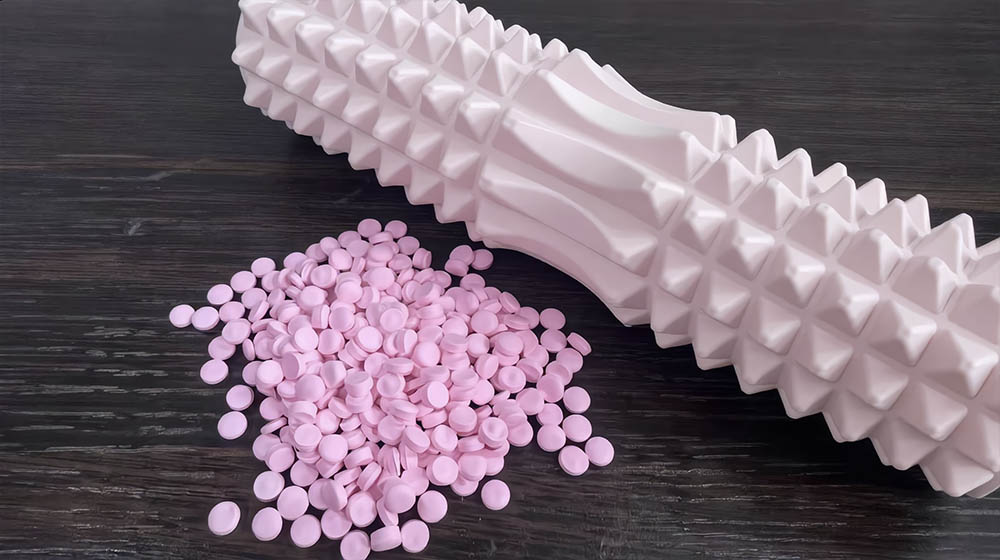
EVA Compound For Eva Foam Roller
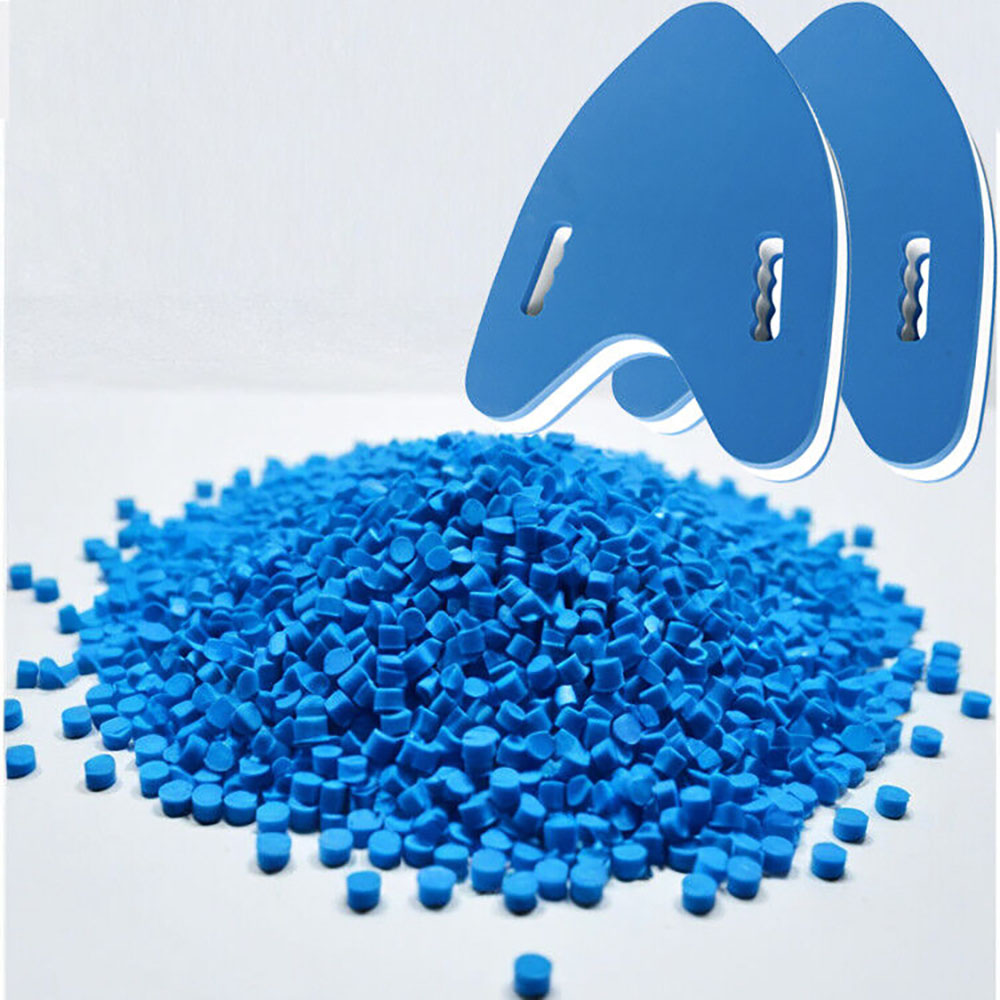
EVA compound for foam rollers requires superior compression recovery performance with fine and uniform foam structure. The smooth surface delivers a comfortable touch while maintaining long-lasting durability without deformation. The finished product is impact and fatigue resistant, withstanding high-frequency compression and rolling use. Ideal for yoga foam rollers, fitness massage rollers, physiotherapy rollers, and more.
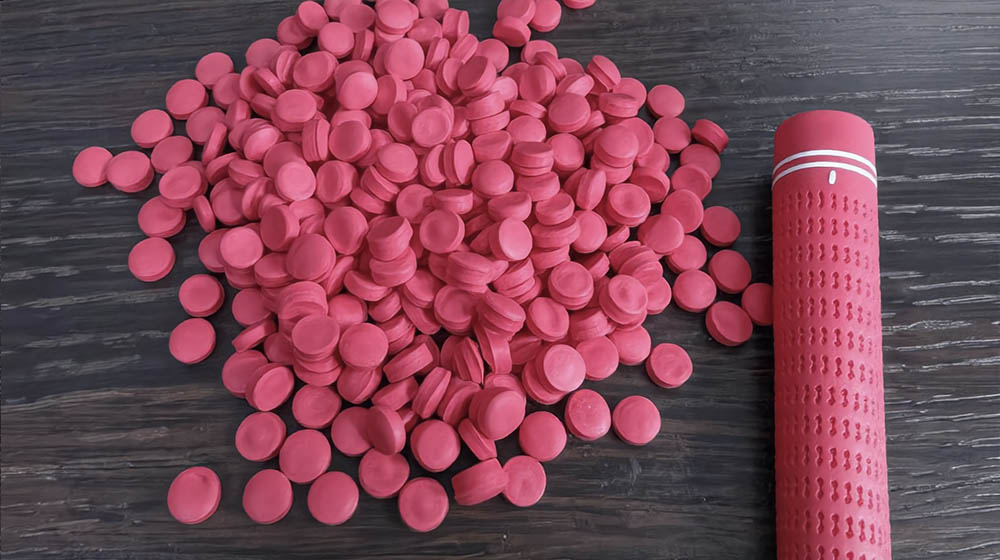
EVA Compound for Sports Equipment Accessories
EVA compound for sports equipment accessories requires superior grip feel, shock absorption, and abrasion resistance with long-lasting durability. The surface delivers a comfortable touch with excellent sweat and slip resistance, preventing hardening or cracking even after prolonged use. Hardness can be flexibly adjusted to meet specific accessory requirements. Ideal for golf club grips, tennis racket handles, baseball bat grips, gym equipment handles, and more.
EVA Material For Boots
EVA compound for boots delivers exceptional compressive strength, withstanding sustained pressure and deformation from boot shaft structures. Outstanding abrasion, oil, and hydrolysis resistance ensures reliable performance in harsh environments such as moisture and oil exposure. The finished product maintains a firm and structured shape without collapsing or deforming. Ideal for industrial boots, rain boots, outdoor boots, snow boots, and more.
Modified EVA Masterbatch: VA Content Dictates the Modification Strategy
VA (Vinyl Acetate) is the key functional monomer in EVA copolymer, and its content directly governs hardness, flexibility, transparency, and polarity. At 3% VA, the material behaves like LDPE — high hardness, strong abrasion resistance. At 40% VA, it performs like an elastomer — soft, transparent, with excellent low-temperature resistance. This broad performance spectrum means the technical strategy for both color masterbatch and EVA masterbatch must be tailored to VA content.
Color Masterbatch & Modified EVA for Masterbatch Low-VA Systems: The Sweet Spot of Cost and Performance
Low-VA EVA (3%-10%) as a carrier for EVA masterbatch combines the processability of LDPE with moderate polarity, making it the most cost-effective segment for both EVA color masterbatch and EVA modified masterbatch. Practical masterbatch types include black, white, color, flame retardant, UV resistant, antistatic, filler, and EVA-g-MAH grafted masterbatch, widely used in footwear, industrial parts, window seals, electronic cables, and cost-reduced filled products. On the modification side, applications cover foam crosslinked footwear, elastomer-blended flexible hoses, and PA/polyester toughening.
Color Masterbatch & Modified EVA Masterbatch for Medium-VA Systems: The Balanced Performer from 10% to 20%
Medium-VA EVA (10%-20%) offers an optimal balance of flexibility and strength, making it the most well-rounded performance range. Practical masterbatch types include black, white, color, flame retardant, UV resistant, high-dispersion masterbatch, and EVA-carrier-specific color masterbatch, widely used in sports shoe midsoles, children’s toys, window and door seals, and cushion packaging. On the modification side, applications cover elastomer-blended foam sheets, crosslinked cushioning materials, and functional filler-reinforced systems. With its balanced polarity, medium-VA serves as the ideal transitional carrier between low-VA and high-VA ranges, offering both processing latitude and performance headroom.
High-VA EVA: Mastering Color Masterbatch & Modification Masterbatch at 20%-40% VA
High-VA EVA (20%-40%) features high polarity, softness, and transparency, making it the most technically demanding range. Practical masterbatch types center on EVA-carrier-specific color masterbatch, high-transparency masterbatch, EVA-g-MAH grafted masterbatch, and functional masterbatch, widely used in food packaging film, medical IV tubing, hot melt adhesives, and cable semi-conductive shielding layers.
EVA Masterbatch Classification by MFI: Performance, Applications & Dosage
EVA Masterbatch is commonly classified by Melt Flow Index (MFI), one of the most important parameters for selecting the right grade. High MFI masterbatches flow quickly, enabling faster production cycles and better dispersion, making them ideal for film blowing, injection molding and high-concentration colorants. Low MFI masterbatches offer higher mechanical strength and melt strength, suiting extrusion, pipe, sheet and foaming applications. Each class requires specific carrier matching, addition levels and dispersion strategies.
High MFI EVA Masterbatch: Best Applications for Film, Injection & Concentrates
High MFI EVA Masterbatch flows quickly and disperses pigments evenly, making it the preferred choice for three key applications. In film blowing and casting, it produces thin, uniform films with smooth, glossy surfaces. In injection molding, it fills thin-wall and small precision parts fast, minimizing flash and shortening cycle times. In color concentrates themselves, a high-flow carrier with high pigment loading ensures outstanding dispersion. For best results, the carrier’s Melt Flow Index should be equal to or higher than the base resin, addition levels typically range from 1% to 3%, and transparent or high-gloss colors show the most obvious effect.
Low MFI EVA Masterbatch: High-Strength Applications & Dispersion Solutions
Low MFI EVA Masterbatch provides higher mechanical strength, toughness and melt strength, making it the preferred choice for demanding applications. In extrusion, it ensures stable, continuous production of sheets, pipes and profiles with excellent dimensional accuracy. In compression molding, high melt strength prevents large and foamed sheets from collapsing. In foaming, slow bubble growth creates uniform cells with a controllable expansion ratio. However, the high viscosity of low MFI base resins makes pigment dispersion more difficult. Practical solutions include using a high MFI carrier or pre-dispersed masterbatch, raising addition levels to 2%–4% (higher for dark colors)
Functional EVA Masterbatch Types: From Coloring to Medical & Toy Grade
Functional EVA Masterbatch goes beyond simple coloring by adding specialized additives that solve real performance challenges. For everyday products, color masterbatch delivers reliable black, white and full-color grades. UV resistant grades protect outdoor items from yellowing; halogen-free flame retardant grades help cables and electronics meet UL94 V-0; foaming masterbatches support shoe midsoles and mats; antistatic and conductive grades protect electronics packaging; antibacterial grades keep medical and daily products hygienic. For the most demanding uses, medical grade masterbatch meets USP Class VI and ISO 10993 biocompatibility, while toy grade masterbatch complies with EN 71-3 safety limits.
EVA Color Masterbatch: Black, White & Full-Color Grades
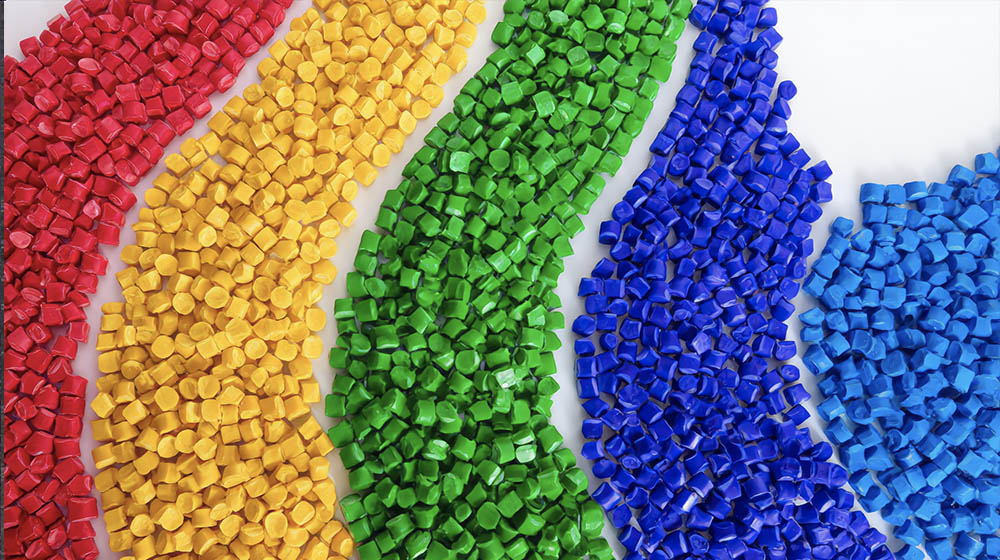
EVA Color Masterbatch provides black, white and full-color grades for all EVA products — footwear, film and toys — with high dispersion, no color specks and no migration as the basic quality threshold.
UV Resistant EVA Masterbatch: Anti-Yellowing Grades
UV Resistant EVA Masterbatch combines UV absorbers and HALS light stabilizers with pigments to prevent yellowing and aging, extending the service life of outdoor footwear, cables and toys under prolonged sunlight.
Flame Retardant EVA Masterbatch: Halogen-Free UL94 V-0
Flame Retardant EVA Color Masterbatch uses halogen-free additives such as ATH and MDH to help EVA compounds reach UL94 V-0, making it the right choice for cables, electronics housings and building materials with RoHS-compliant export requirements.
EVA Foam Masterbatch: Co-Foaming Colors
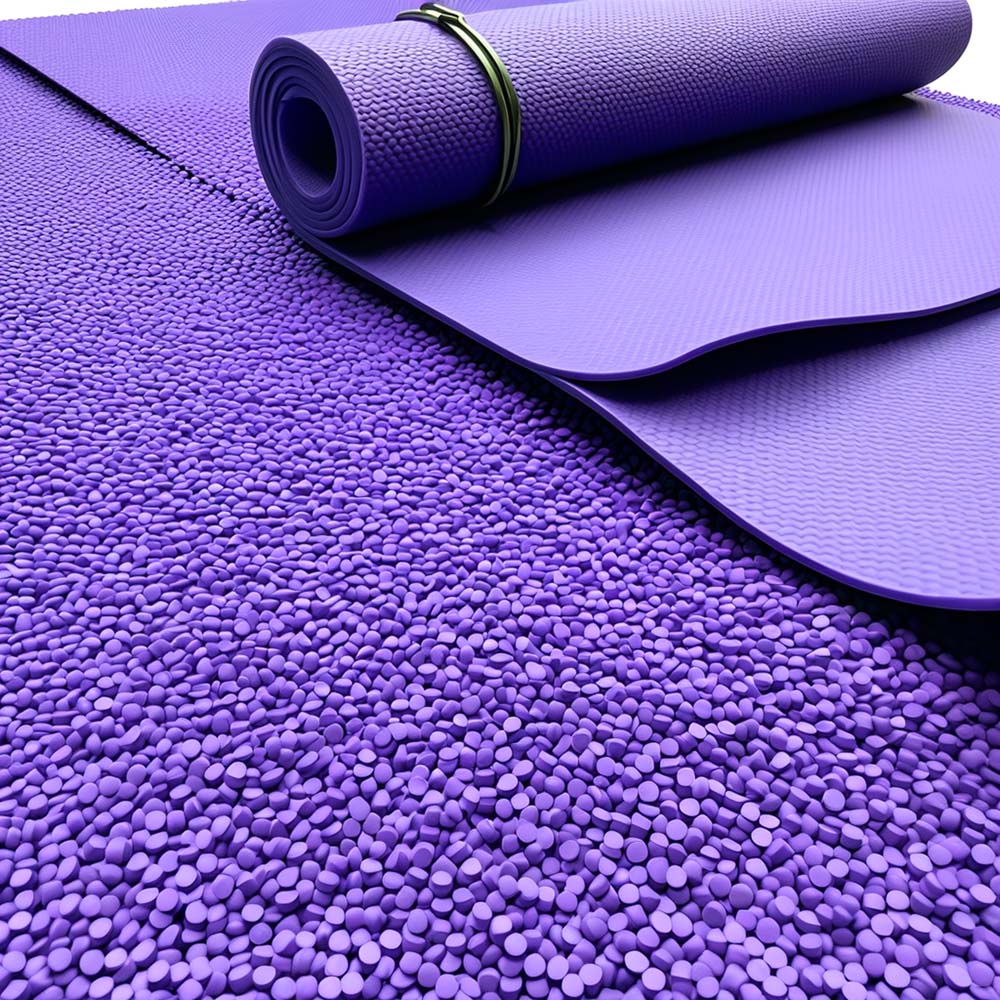
VA Foam Masterbatch colors while co-foaming, never suppressing AC blowing agents. It ensures uniform cells with a closed-cell ratio above 90%, making it ideal for shoe midsoles, kids’ mats, yoga mats and cushioning packaging.
Antistatic & Conductive EVA Masterbatch
Antistatic & Conductive EVA Masterbatch eliminates static buildup via conductive carbon black or internal antistatic agents, achieving surface resistance of 10⁶–10⁹Ω for electronics packaging, explosion-proof products and medical tubing.
Antibacterial EVA Masterbatch
Antibacterial EVA Masterbatch incorporates silver-ion or zinc antibacterial agents with 99%+ efficacy, stable at 200°C processing temperatures, ideal for medical tubing, children’s toys and odor-resistant footwear.
Medical Grade EVA Masterbatch
Medical Grade EVA Masterbatch uses medical-grade EVA and high-purity pigments free of heavy metals, PAHs and phthalates, meeting USP Class VI and ISO 10993 biocompatibility for infusion lines, catheters and blood bags.
Toy Grade EVA Masterbatch
Toy Grade EVA Masterbatch uses non-toxic pigments free of heavy metals, azo dyes and phthalates, complying with EN 71-3, ASTM F963 and CPSIA for children’s mats, puzzles and flotation toys.
Special Effect EVA Masterbatch
Special Effect EVA Masterbatch delivers pearlescent, glow-in-the-dark, scented and thermal conductive effects, adding premium value to fashion footwear, decorative toys and specialty insoles.